The IBA recycling Plant upgrade in Jingmen, Hubei has been successfully completed into a more efficient, intelligent and standardized recycling system in less than two months—from process design to commissioning.
The project focused on replacing outdated equipment, rebuilding the sorting process and introducing a more intelligent control system. The upgrade significantly improved processing capacity, metal recovery, operating efficiency and environmental performance.
From an Outdated Sorting Line to a Modern IBA Recycling System
The original production line relied on a traditional and relatively simple sorting process with limited equipment configurations. After years of operation, several problems became increasingly evident:
- Limited processing capacity
- Low sorting efficiency
- Insufficient metal recovery
- Significant material loss
- High dependence on manual operation
- Frequent equipment failures
- Increasing operating and maintenance costs

More importantly, the existing process could no longer fully utilize the valuable resources contained in Incineration Bottom Ash (IBA).
Rather than making isolated equipment replacements, the project adopted a system-level upgrade approach.
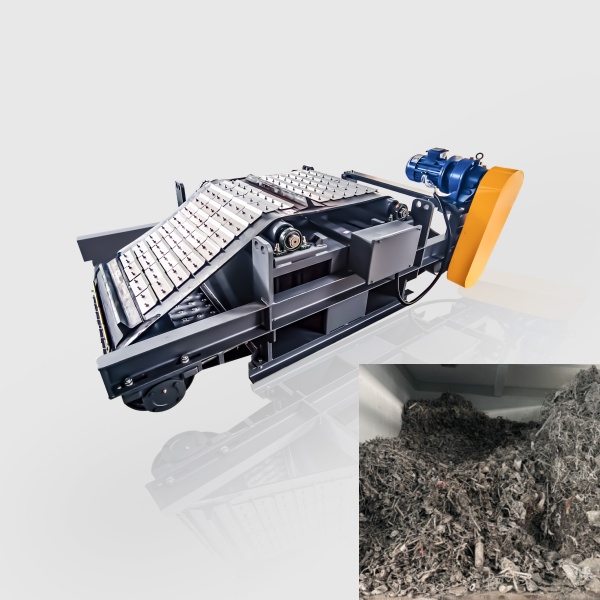
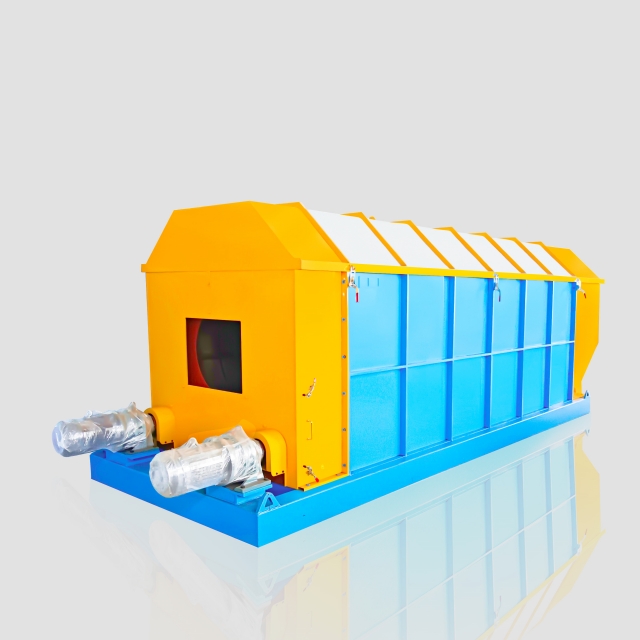
The original process was redesigned, outdated equipment was removed, and specialized sorting equipment was added to create a more efficient and refined IBA recycling process.
Rebuilding the Process for More Efficient Sorting
One of the key objectives of the project was to overcome the limitations of the original simple sorting configuration.
The upgraded line introduced a more systematic equipment combination and optimized the material flow through different processing stages.
Instead of relying on a single sorting method, the upgraded system uses specialized equipment according to different material characteristics and recovery requirements.
This enables the production line to achieve better control over:
- Material processing
- Particle classification
- Metal separation
- Resource recovery
- Production stability
The result is a more coordinated sorting process designed to maximize the value recovered from IBA.

Upgrading Equipment and Intelligent Control
The project did not simply add new machines. It also upgraded the overall control system.
A more intelligent control system was introduced to improve production monitoring and equipment coordination, helping operators manage the line more efficiently.
The upgrade supports a transition from a traditional equipment-oriented production model toward a more intelligent, standardized and automated operation mode.
This reduces dependence on manual intervention while improving the consistency of production.
Key Results of the IBA Recycling Plant Upgrade
The most important measure of an equipment upgrade is its actual production performance.
According to the project results, the upgraded Jingmen IBA recycling line achieved significant improvements.
2× Higher Processing Capacity
The processing capacity was doubled, allowing the plant to handle substantially more IBA within the same production operation.
This provides greater production flexibility and improves the overall utilization of the recycling facility.
42% Higher Metal Recovery
The optimized sorting process increased the metal recovery rate by 42%.
More valuable ferrous and non-ferrous metals can now be recovered from the IBA stream, reducing resource loss and increasing the economic value of the material.
51% Higher Resource Utilization
Improved separation accuracy and process coordination increased the overall resource utilization rate by 51%.
This means more valuable materials can be recovered and redirected into useful applications instead of being lost as waste.
38% Lower Labor Costs
The upgraded production line reduced manual operating requirements, resulting in a 38% reduction in labor costs.
At the same time, improved equipment coordination and process stability helped reduce equipment-related failures and maintenance pressure.

Improving Production Quality and Environmental Performance
The upgrade also focused on more than recovery efficiency.
By reorganizing the production process and introducing standardized operating procedures, the project improved the overall management of the recycling line.
The upgraded system provides improvements in:
Processing efficiency
Higher throughput and better material handling.
Sorting quality
More precise recovery of valuable metals.
Operational stability
Reduced equipment failure and manual intervention.
Environmental performance
Improved process management and environmental compliance.
Production standardization
A more structured and controlled production process.
The overall production line has moved toward a more intelligent, standardized and environmentally responsible operation model.
A Complete Upgrade in Less Than Two Months
One of the highlights of the Jingmen project was the implementation period.
From process design to on-site implementation and commissioning, the complete upgrade was completed in less than two months.
This required close coordination between process design, equipment manufacturing, site installation, system integration and commissioning.
The project demonstrates that upgrading an existing IBA recycling line does not necessarily require building an entirely new plant.
With a suitable process design and equipment configuration, an existing production line can be transformed to achieve significantly higher processing and recovery performance.
What This IBA Recycling Project Demonstrates
The Jingmen project highlights an important trend in the IBA recycling industry:
The value of an existing recycling line can often be unlocked through systematic upgrading rather than simply adding more equipment.
For plants facing aging equipment, insufficient capacity, low recovery rates or high operating costs, a targeted upgrade can address multiple problems simultaneously.
The key is to evaluate the existing production line, identify the main bottlenecks and redesign the process around actual material and production requirements.
Conclusion
Modern IBA recycling is moving toward higher efficiency, smarter operation and greater resource value.
For aging facilities, a systematic upgrade provides a practical way to adapt existing infrastructure to new production and environmental requirements while unlocking more value from waste resources.